Table of Contents
Woven Shirt Sewing Production Line Layout in Apparel Industry
Machine layout plan is always a key factor for higher production. If the total plan is executed perfectly then it will easy for the production team to meet shipment date without any hassle. As its importance, this article has presented a well-tested machine layout plan for woven shirt or formal shirt or casual shirt or basic shirt.
You may follow:
1. Major Components of a Basic Shirt | Operation Breakdown of a Basic Shirt
2. Different Parts of a Jeans Pant | Operation Breakdown of Jeans Pant
3. How to Setup Machine Lay Out for Jeans Pant in Apparel Industry?
4. Cutting Cost Calculation Formula | Fabric Cutting Cost in Bangladesh
5. Apparel Checking Methods | Quality Checking List of Apparel Industry
6. Apparel Packing Materials | Apparel Packaging Cost Calculation Formula
7. What is Shipment | What is Shipping | International Shipping Process Flow Chart
8. Steps of Apparel Inspection | Apparel Inspection Cost
9. What is Bra or Brassier? | 35 Different Types of Bra with Names and Pictures
10. List of Top 100 Clothing Brands in the World
Machine Layout for Woven Shirt in Apparel Manufacturing Sector
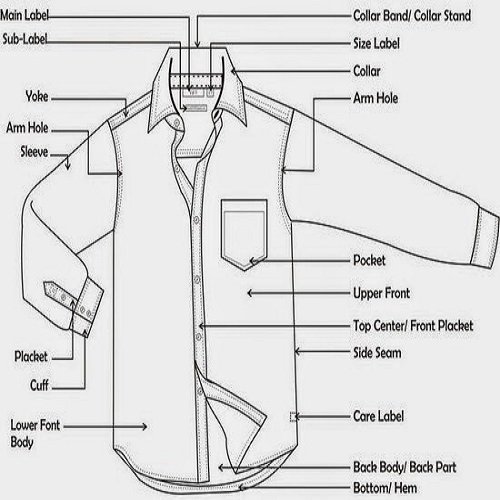
We will make calculations for body and collar-cuffs-sleeves separately @150pc per hour. Body processes operations are shown here. Processes are allocated to operators so as to make a layout for body processes.
Machine Lay Out Plan for Shirt Body
| SL No. | Name of Operations | Machine Required | Standard Time | Operator Allocation |
| 01 | Attach top center to left front | 4-ndl double chain stitch machine | 24” | Operator-1 |
| 02 | Hem pocket mouth | 1-ndl lock stitch with thread trimmer | 12” | Operator-2,3 |
| 03 | Fold pocket | Manual | 42” | Operator-4,5 |
| 04 | Attach pocket | 1-ndl lock stitch with thread trimmer | 40” | Operator-2,3 |
| 05 | Hem right front button stand | 1-ndl lock stitch with hemmer folder | 24” | Operator-6 |
| 06 | Cut & fold label | Label cutting & folding machine | 3” | Operator-7 |
| 07 | Attach label to under yoke | 1-ndl lock stitch with thread trimmer | 16” | Operator-7 |
| 08 | Back yoke attach sewing | 1-ndl lock stitch with thread trimmer | 24” | Operator-8 |
| 09 | Back yoke top stitch | 1-ndl lock stitch with thread trimmer | 19” | Operator-9 |
| 10 | Shoulder join | 1-ndl lock stitch with thread trimmer | 46” | Operator-10, 11 |
| 11 | Top stitch on shoulder join | 1-ndl lock stitch with thread trimmer | 24” | Operator-12 |
| 12 | Attach sleeves | 2-ndl 5-thread safety stitcher | 48” | Operator-13, 14 |
| 13 | Side seam | 2-ndl feed of the arm machine | 46” | Operator-15, 16 |
| 14 | Collar attach sew | 1-ndl lock stitch with thread trimmer | 40” | Operator-17, 18 |
| 15 | Collar attach stitch | 1-ndl lock stitch with thread trimmer | 40” | Operator-19, 20 |
| 16 | Hem body bottom | 1-ndl lock stitch with thread trimmer with hemmer foot | 24” | Operator-21 |
| 17 | Attach cuffs | 1-ndl lock stitch with cuff folder | 48” | Operator-22, 23 |
| 18 | Button sewing | Button sewing machine | 38” | Operator-24, 25 |
| 19 | Buttonhole sewing | Buttonhole sewing machine | 36” | Operator-26, 27 |
| Total standard time for body processes | 594” | |||
Average Process Time Calculation Method
Average process time,
= (594/19)
= 31.26”
Calculation of BPT, UCL, LCL, Organization Efficiency & Production Target Per Hour
Production target per hour with 27 operators,
= {(27×3600×0.85)/594}
= 139pcs per hour
Again,
Bottleneck time= 26 second,
So,
Production per hour,
= (3600/26)
= 138pcs per hour.
Now,
Basic pitch time (BPT) is,
= (594/27)
= 22”
Again,
Upper control limit (UCL) is,
= (22”/0.85)
= 25.88”
Again,
Lower control limit (LCL) is,
= {2 × (BPT-UCL)}
= (44-25.88”)
= 18.12”
Now,
Organization efficiency is,
= (BPT/Bottleneck time)
= {(22”/26”) × 100}
= 84.66%
Again,
Direct productivity is,
= (138/27)
= 5.11 pcs per operator per hour
Machine Lay Out Plan for Shirt Collar, Cuffs and Sleeves
| SL No. | Name of Operations | Machine Required | Standard Time | Operator Allocation |
| Collar Processes | ||||
| Fp-1 | Fuse interlining | Fusing press | 6” | Operator-Fp-1 |
| Clr-2 | Sew collar | 1-ndl lock stitch with thread trimmer | 24” | Operator-1 |
| Clr-3 | Cut collar tip & turn | Manual | 22” | Operator-2 |
| Clr-4 | Form collar | Collar forming machine | 20” | Operator-3 |
| Clr-5 | Press collar | Manual | 20” | Operator-4 |
| Clr-6 | Top stitch collar | 1-ndl lock stitch with thread trimmer | 16” | Operator-5 |
| Clr-7 | Sew collar bottom | 1-ndl lock stitch with thread trimmer | 8” | Operator-5 |
| Clr-8 | Trim collar bottom | Collar contour trimmer | 6” | Operator-6 |
| Fp-1 | Fuse interlining to band | Fusing press | 6” | Operator-Fp-1 |
| Clr-9 | Feel or roll band | 1-ndl lock stitch with thread trimmer | 18” | Operator-6 |
| Clr-10 | Collar band attach sewing | 1-ndl lock stitch with thread trimmer | 24” | Operator-7 |
| Clr-11 | Turn band | Manual | 10” | Operator-8 |
| Clr-12 | Collar band attach stitch | 1-ndl lock stitch with thread trimmer | 18” | Operator-9 |
| Clr-13 | Cut band bottom | Over lock machine | 6v | Operator-9 |
| Clr-14 | Mark 3-point on collar | Manual | 12” | Operator-8 |
| Cuff Processes | ||||
| Fp-1 | Fuse interlining | Fusing press | 12” | Operator-Fp-1 |
| Cf-2 | Fell or roll cuff | 1-ndl lock stitch with thread trimmer | 18” | Operator-10, 11 |
| Cf-3 | Sew or run stitch cuffs | 1-ndl lock stitch with thread trimmer | 30” | Operator-10, 11 |
| Cf-4 | Fold inside | Iron or vacuum board | 8” | Operator-12 |
| Cf-5 | Turn cuffs | Manual or iron | 12” | Operator-12 |
| Cf-6 | Form cuffs | Cuff forming machine | 24” | Operator-13 |
| Cf-7 | Top stitch cuffs | 1-ndl lock stitch with thread trimmer | 18” | Operator-14 |
| Cf-8 | Cuff pair match | Manual | 6” | Operator-15 |
| Sleeve Processes | ||||
| Slv-1 | Sew under placket to sleeve | 1-ndl lock stitch with thread trimmer | 18” | Operator-15 |
| Slv-2 | Fold upper placket | Manual | 24” | Operator-16 |
| Slv-3 | Attach sleeve placket | 1-ndl lock stitch with thread trimmer | 36” | Operator-17, 18 |
| Total standard time for collar, cuff & sleeves | 422” | |||
Average Process Time Calculation Method:
Average process time,
= (422/24)
= 17.58”
Calculation of BPT, UCL, LCL, Organization Efficiency & Production Target Per Hour
Production target per hour with 19 operators,
= {(19×3600×0.85)/422}
= 143pcs per hour
Again,
Bottleneck time= 24 seconds,
So,
Production per hour is,
= (3600/24)
= 150pcs per hour
Now,
Basic pitch time (BPT) is,
= (422/19)
= 22.21”
Again,
Upper control limit (UCL) is,
= (22.21”/0.85)
= 26.13”
Again,
Lower control limit (LCL) is,
= {2 × (BPT-UCL)}
= (44.42-26.13”)
= 18.29”
Now,
Organization efficiency is,
= (BPT/Bottleneck time)
= {(22.21”/24”) × 100}
= 97.66%
Again,
Direct productivity is,
= (150/18)
= 8.33 pcs per operator per hour